Laser settings for cardboard and paper
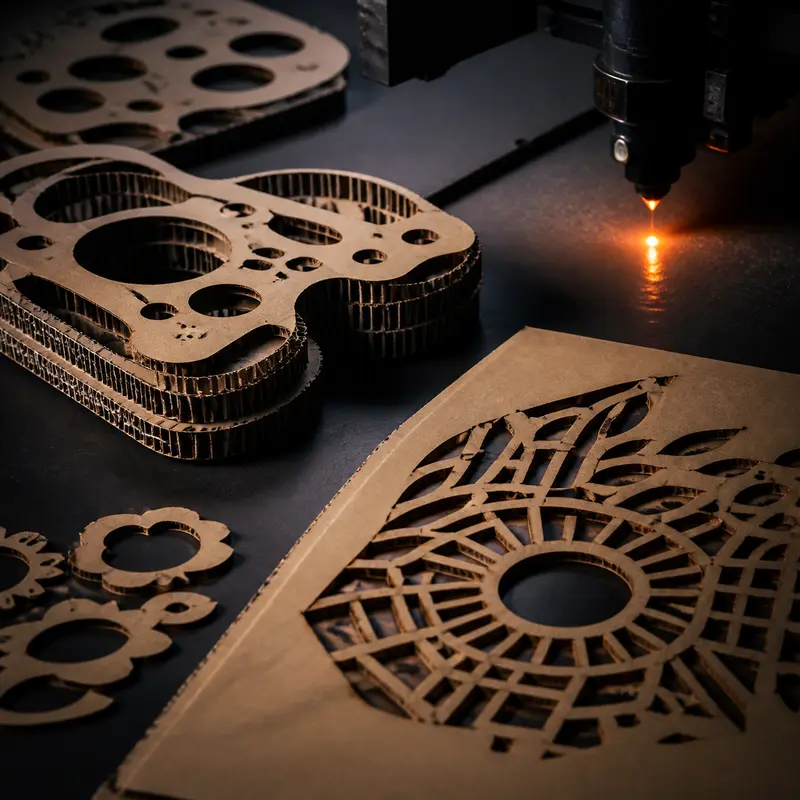
Paper and cardboard cut on very little energy — and catch fire on very little too. Corrugated board adds hollow flutes between its liners. Here are the maker numbers, and the habits that keep a cardboard job from turning into a fire.
 Before you start With care
- Never leave it running. Paper and cardboard cut well but catch fire easily (what not to laser cut). Trotec says a laser should never be left unattended, with an extinguisher within easy reach.
- The maker flags it too. TwoTrees’ test list marks cardboard cutting on one of its machines with a fire warning.
- Air assist on, bed clean. Air assist blows away dust and smoke that could ignite, and cutting residues left in the machine can catch fire (Trotec).
- Heavy smoke. In a 2024 desktop CO2 study, cardboard gave the highest respirable particle level of the four materials tested and 23.9 ppm carbon monoxide inside the unventilated chamber (O’Neill 2024). Run your extraction (exhaust fan calculator).
- Plastic-laminated board is not paper. A board with a plastic film or coating is a plastics job; find out what it is first.
 What the beam does
Switch the material or laser and watch the same beam give a different result.
- Kraft liner
- Browned fibres
- Kraft paper 0.6 mm
- Cut through in a fast pass
- Liners
- Hollow flutes
- Kerf
- Corrugated board
- Flame in the flutes and at the edge
The top fibres brown and char. Kraft engraves on very little energy — some maker rows put about 0.01 J into each mm of line.
Cross-section, not to scale.
 Which laser can process it
These are this material’s rows from our diode vs CO2 vs fiber matrix. (full matrix)
Organic materials are a CO2 job, not fiber.
 Maker settings on one scale
Every value is a starting point published by the maker, and the maker is the source; none of them were tested by us. Machines differ in optical power, so power % and speed are converted to the energy the beam puts into each millimetre of line (J/mm). Tap a point or a table row to see the original row, the math and a link that fills in the converter.
This is the same formula as the converter. Between lasers of the same type, similar J/mm gives a similar burn. Cutting energy rises steeply with thickness, so compare rows of similar thickness.
AtomStack’s “Carton” rows are cardboard (the table does not say corrugated or solid); “Korrugated Cardboard” (sic) appears only for its 55 W CO2 Hurricane. The two Hurricane “Kraft Paper” cuts at 6 and 8 mm cannot be single sheets — probably kraft board — so read them as board. “Office Paper” rows are engraving only. TwoTrees’ 3 mm cardboard cuts are included. The A20 Pro V2 LaserGRBL kraft cut at 10,000 mm/min disagrees with its 1,500 mm/min LightBurn twin and is marked as a likely typo; the A40 Pro V2 LightBurn cut carries an S-value.
| Machine (optical W) | Software | Maker label · thickness | Job | Speed mm/min | Power | Interval | Passes | J/mm | |
|---|---|---|---|---|---|---|---|---|---|
| LightBurn | Kraft Paper | Engrave | 6,000 | 60% | 0.1 | 1 | 0.06 | Convert → | |
| LaserGRBL | Kraft Paper | Engrave | 6,000 | S600 | 0.1 | 1 | 0.06 | Convert → | |
| LightBurn | Office Paper | Engrave | 3,000 | 30% | 0.08 | 1 | 0.06 | Convert → | |
| LaserGRBL | Office Paper | Engrave | 3,000 | S300 | 0.0833 | 1 | 0.06 | Convert → | |
| LightBurn | Carton | Engrave | 5,000 | 60% | 0.1 | 1 | 0.072 | Convert → | |
| LaserGRBL | Carton | Engrave | 5,000 | S600 | 0.1 | 1 | 0.072 | Convert → | |
| LightBurn | Kraft Paper | Engrave | 10,000 | 30% | 0.08 | 1 | 0.036 | Convert → | |
| LightBurn | Kraft Paper · 0.6 | Cut | 1,500 | 80% | — | 1 | 0.64 | Convert → | |
| LaserGRBL | Kraft Paper | Engrave | 10,000 | S300 | 0.0833 | 1 | 0.036 | Convert → | |
| LaserGRBL | Kraft Paper · 0.6mm | Cut | 10,000 | S800 ? | — | 1 | 0.096 | Convert → | |
| LightBurn | Office Paper | Engrave | 20,000 | 70% | 0.08 | 1 | 0.042 | Convert → | |
| LaserGRBL | Office Paper | Engrave | 20,000 | S700 | 0.0833 | 1 | 0.042 | Convert → | |
| LightBurn | Carton | Engrave | 3,000 | 80% | 0.08 | 1 | 0.32 | Convert → | |
| LaserGRBL | Carton | Engrave | 3,000 | S800 | 0.0833 | 1 | 0.32 | Convert → | |
| LightBurn | Kraft Paper | Engrave | 30,000 | 20% | 0.1 | 1 | 0.0096 | Convert → | |
| LightBurn | Kraft Paper · 0.6 | Cut | 2,000 | 80% | — | 1 | 0.576 | Convert → | |
| LaserGRBL | Kraft Paper | Engrave | 30,000 | S200 | 0.1 | 1 | 0.0096 | Convert → | |
| LaserGRBL | Kraft Paper · 0.6 | Cut | 2,000 | S800 | — | 1 | 0.576 | Convert → | |
| LightBurn | Office Paper | Engrave | 20,000 | 80% | 0.1 | 1 | 0.0576 | Convert → | |
| LaserGRBL | Office Paper | Engrave | 20,000 | S800 | 0.1 | 1 | 0.0576 | Convert → | |
| LightBurn | Carton | Engrave | 30,000 | 50% | 0.1 | 1 | 0.024 | Convert → | |
| LaserGRBL | Carton | Engrave | 30,000 | S500 | 0.1 | 1 | 0.024 | Convert → | |
| LightBurn | Kraft Paper | Engrave | 30,000 | 20% | 0.1 | 1 | 0.0096 | Convert → | |
| LightBurn | Kraft Paper · 0.6 | Cut | 2,000 | 80% | — | 1 | 0.576 | Convert → | |
| LaserGRBL | Kraft Paper | Engrave | 30,000 | S200 | 0.1 | 1 | 0.0096 | Convert → | |
| LaserGRBL | Kraft Paper · 0.6 | Cut | 2,000 | S800 | — | 1 | 0.576 | Convert → | |
| LightBurn | Office Paper | Engrave | 20,000 | 80% | 0.1 | 1 | 0.0576 | Convert → | |
| LaserGRBL | Office Paper | Engrave | 20,000 | S800 | 0.1 | 1 | 0.0576 | Convert → | |
| LightBurn | Carton | Engrave | 30,000 | 50% | 0.1 | 1 | 0.024 | Convert → | |
| LaserGRBL | Carton | Engrave | 30,000 | S500 | 0.1 | 1 | 0.024 | Convert → | |
| LightBurn | Kraft Paper | Engrave | 10,000 | 40% | 0.08 | 1 | 0.115 | Convert → | |
| LightBurn | Kraft Paper · 0.6 | Cut | 2,000 | S800 ? | — | 1 | 1.15 | Convert → | |
| LaserGRBL | Kraft Paper | Engrave | 10,000 | 40% | 0.0833 | 1 | 0.115 | Convert → | |
| LaserGRBL | Kraft Paper · 0.6mm | Cut | 2,000 | S800 | — | 1 | 1.15 | Convert → | |
| LightBurn | Office Paper | Engrave | 10,000 | 47% | 0.1 | 1 | 0.135 | Convert → | |
| LaserGRBL | Office Paper | Engrave | 10,000 | 47% | 0.1 | 1 | 0.135 | Convert → | |
| LightBurn | Carton | Engrave | 10,000 | 35% | 0.08 | 1 | 0.101 | Convert → | |
| LaserGRBL | Carton | Engrave | 10,000 | 35% | 0.0833 | 1 | 0.101 | Convert → | |
| LightBurn | Kraft Paper | Engrave | 9,000 | 30% | 0.1 | 1 | 0.14 | Convert → | |
| LightBurn | Kraft Paper · 0.6 | Cut | 9,000 | 90% | — | 1 | 0.42 | Convert → | |
| LaserGRBL | Kraft Paper | Engrave | 9,000 | S300 | 0.1 | 1 | 0.14 | Convert → | |
| LaserGRBL | Kraft Paper · 0.6 | Cut | 9,000 | S900 | — | 1 | 0.42 | Convert → | |
| LightBurn | Office Paper | Engrave | 10,000 | 27% | 0.1 | 1 | 0.113 | Convert → | |
| LaserGRBL | Office Paper | Engrave | 10,000 | S270 | 0.1 | 1 | 0.113 | Convert → | |
| LightBurn | Carton | Engrave | 8,000 | 25% | 0.1 | 1 | 0.131 | Convert → | |
| LaserGRBL | Carton | Engrave | 8,000 | S250 | 0.1 | 1 | 0.131 | Convert → | |
| Bitmap | Kraft Paper | Engrave | 24,000 | 40% | 0.1 | 1 | 0.055 | Convert → | |
| Vector Line | Kraft Paper | Engrave | 3,500 | 5% | — | 1 | 0.0471 | Convert → | |
| - | Kraft Paper · 8mm | Cut | 300 | 100% | — | 1 | 11 | Convert → | |
| - | Kraft Paper · 6mm | Cut | 250 | 80% | — | 1 | 10.6 | Convert → | |
| Bitmap | Korrugated Cardboard | Engrave | 24,000 | 30% | 0.1 | 1 | 0.0413 | Convert → | |
| Vector Line | Korrugated Cardboard | Engrave | 3,500 | 6% | — | 1 | 0.0566 | Convert → | |
| - | Korrugated Cardboard · 6mm | Cut | 800 | 60% | — | 1 | 2.48 | Convert → | |
| Bitmap | Kraft Paper | Engrave | 9,000 | 80% | 0.08 | 1 | 0.0267 | Convert → | |
| Vector Line | Kraft Paper | Engrave | 1,000 | 15% | — | 1 | 0.045 | Convert → | |
| Bitmap | Carton | Engrave | 8,000 | 65% | 0.08 | 1 | 0.0244 | Convert → | |
| Vector Line | Carton | Engrave | 1,000 | 15% | — | 1 | 0.045 | Convert → | |
| LightBurn | Kraft Paper · 0.6mm | Cut | 700 | 80% | — | 1 | 0.343 | Convert → | |
| LightBurn | Carton · 6mm | Cut | 150 | 80% | — | 1 | 1.6 | Convert → | |
| Bitmap | Kraft Paper | Engrave | 20,000 | 80% | 0.08 | 1 | 0.048 | Convert → | |
| Vector Line | Kraft Paper | Engrave | 500 | 6% | — | 1 | 0.144 | Convert → | |
| - | Kraft Paper · 0.6mm | Cut | 1,500 | 80% | — | 1 | 0.64 | Convert → | |
| Bitmap | Office Paper | Engrave | 18,000 | 80% | 0.08 | 1 | 0.0533 | Convert → | |
| Bitmap | Carton | Engrave | 20,000 | 80% | 0.1 | 1 | 0.048 | Convert → | |
| Vector Line | Carton | Engrave | 500 | 6% | — | 1 | 0.144 | Convert → | |
| - | Carton · 6mm | Cut | 600 | 80% | — | 1 | 1.6 | Convert → | |
| - | 3 mm cardboard · 3mm | Cut | 300–400 | 100% | — | 1 | 0.943 | Convert → | |
| - | 3 mm cardboard · 3mm | Cut | 800 | 100% | — | 1 | 0.75 | Convert → |
 Why cardboard catches fire
Focus and a clean lensAn out-of-focus beam is MatEdU’s main exception to paper’s low ignition risk
 Air assist and exhaust on
Blows away smoke and dust (Trotec); stale air makes soot that overheats the spot (MatEdU)
 Clean bed and tray
Leftover residue can catch fire (Trotec)
Extinguisher, fire blanket, and stayNever leave it running (Trotec, MatEdU)
In the lists we track, paper and cardboard carry the same warning: they cut well but catch fire easily (what not to laser cut). Trotec’s fire article lists the usual causes of laser fires: wrong power settings, and dust and cutting residues left inside the machine. MatEdU adds an important nuance: paper does not conduct heat well, so the risk of it reaching its flashpoint away from the laser spot is very low — the exceptions are a beam that is out of focus and air in the machine that is not vented properly. Starved of air, the burn makes soot and smoke that cloud the beam and overheat the spot (MatEdU). Corrugated board stacks two liners around hollow flutes, so a cut passes through paper, air, paper.
- Lowest energy that cuts through. Compare your row with the maker rows below before you add power.
- Focus on the top face and keep the lens clean (MatEdU).
- Air assist and exhaust on for cuts (Trotec, MatEdU).
- Clean the bed and tray before every job (Trotec).
- Extinguisher and fire blanket in reach, and stay with it (Trotec, MatEdU, Stanford EH&S).
Kraft paper, office paper and corrugated board
On the J/mm scale, paper is the cheapest material on this site. AtomStack’s diode kraft fill (raster) engravings put about 0.01–0.14 J into each mm of line, and its office-paper fill engravings 0.04–0.14. Cutting 0.6 mm kraft takes about 0.34–1.15 J/mm; 3–6 mm cardboard about 0.75–1.6 J/mm on the diodes and 2.5 J/mm on the 55 W CO2 (chart). For comparison, 3 mm plywood cuts at roughly 0.9–1.7 J/mm in the plywood & basswood rows — so cardboard is not much cheaper to cut than thin plywood, only quicker to burn.
 Engrave the front, cut from the back
Air assist off
Keep it registered on the honeycomb
Air assist on
Trotec’s cardboard chair project (2 mm corrugated board, 30 W CO2) engraves the front, then flips the sheet and cuts it from the back, with the sheet held down on a vacuum table over a honeycomb. Air assist is off for the engraving and on for the cut (Trotec). Its power and speed are percentages of its own machine, so they do not convert to J/mm here — use the method, not the numbers.
Smoke from cardboard
O’Neill and colleagues ran a desktop 40 W CO2 cutter on cardboard, wood, plastic and glass. Cardboard gave the most respirable particles (253.9 mg/m³ inside the chamber with no ventilation) and the smallest ultrafine particles, and carbon monoxide reached 23.9 ppm. With ventilation, respirable particles fell by 61 % on average across the materials, and carbon monoxide fell below the detection limit. These were 5-minute samples inside the machine, not room exposures (O’Neill 2024). Size your fan with the exhaust fan calculator.
How to run a cardboard test
Cardboard tests are short, but every one is a fire test. Do them with the lid closed, the exhaust on and the extinguisher in reach.
- 1
Clean the bed and tray first (Trotec).
- 2
Same board, same batch — flute size and liners differ between boxes.
- 3
Start fast. Cut small squares at a fixed speed, then slow down or add power until they drop out.
- 4
Air assist on for every cut.
- 5
Stay at the machine. If a flame does not go out by itself at once, stop the job. Do not open the lid onto a flame (general practice); keep the extinguisher and a fire blanket within reach (MatEdU).
FAQ
- What are good laser settings for cardboard?
- TwoTrees cuts 3 mm cardboard at 300–400 mm/min and 100 % on a 5.5 W diode and at 800 mm/min on its 10 W TS3. AtomStack cuts 6 mm “carton” at 150 mm/min and 80 % on the 5 W P1 and at 600 mm/min on the 20 W Kraft — about 0.75–1.6 J/mm on these diodes. Its 55 W CO2 cuts 6 mm corrugated at 800 mm/min and 60 % (about 2.5 J/mm).
- What laser settings work for kraft paper?
- AtomStack’s diode kraft fill (raster) engravings run 6,000–30,000 mm/min at 20–80 % with a 0.08–0.1 mm interval (about 0.01–0.14 J/mm per line). Its 0.6 mm kraft cuts run 700–9,000 mm/min at 80–90 % power (about 0.34–1.15 J/mm). Scale a row to your machine and test on the same paper.
- Can a diode laser cut cardboard?
- Yes. Paper and cardboard are cut by both diode and CO2 lasers in the sources behind our laser-type matrix; fiber lasers are not suited. The maker rows here cut 3–6 mm board on 5–20 W diodes.
- How do I stop cardboard catching fire in a laser?
- Use the lowest energy that cuts through, keep air assist on, clean dust and scraps out of the machine before each job, keep an extinguisher within reach, and never leave the machine running (Trotec). MatEdU adds: keep the beam in focus and the machine well vented, and keep a fire blanket by the extinguisher. Stop the job if a flame does not go out at once.
Sources
- AtomStack, Material Setting (LightBurn, LaserGRBL and machine tables)
- TwoTrees, Laser Engraver Material Test List
- Trotec blog (Nadine Schall), Is laser cutting a fire hazard? (2024-09-09)
- Trotec, Cardboard chair (laser project: 2 mm corrugated, Speedy 300)
- O’Neill K, Niu X, Wang J, Fang R. Respirable particles and gas contaminants emissions from a desktop laser cutter and engraver. Aerosol and Air Quality Research 2024;24(8):240032
- MatEdU (NSF-funded), Materials for Laser Cutter Machines
- Stanford EH&S, Laser Cutters Safety Guidance (archived copy)
- LightBurn documentation, Material Test
Sources for the laser-type verdicts
- xTool, Fiber vs CO2 vs Diode Laser: Differences Explained
- xTool Support, xTool F1 Product Introduction
- Glowforge Aura (diode) product page
- Trotec, Diode vs CO2 vs fiber laser comparison guide
- Glowforge Performance Series tech specs (CO2)
- University of Georgia, Laser Cutter Materials List (CO2)
- Rutgers Makerspace, Lasers (CO2 and MOPA fiber)
- xTool Support, Material Tests with the 1064 nm Infrared Module
- Boss Laser, fiber laser materials
Last checked 2026-11-02 · Maker values and calculations; we did not process this material ourselves.